You tin the iron, touch it to the wire, and the solder rolls straight off like water on wax. More heat does not help. More flux does not help. Scrubbing the end with sandpaper sometimes helps and sometimes makes it worse.
The reason is that “enameled wire” is not one material. It is a family of coatings, and only one of them comes off by itself at soldering heat. Everything below hangs on finding out which one you are holding, which takes about five seconds.
What’s Inside!
The Five-Second Test
Melt a blob of solder on the iron tip and hold a scrap end of the wire in it for three to five seconds. Watch what the solder does.
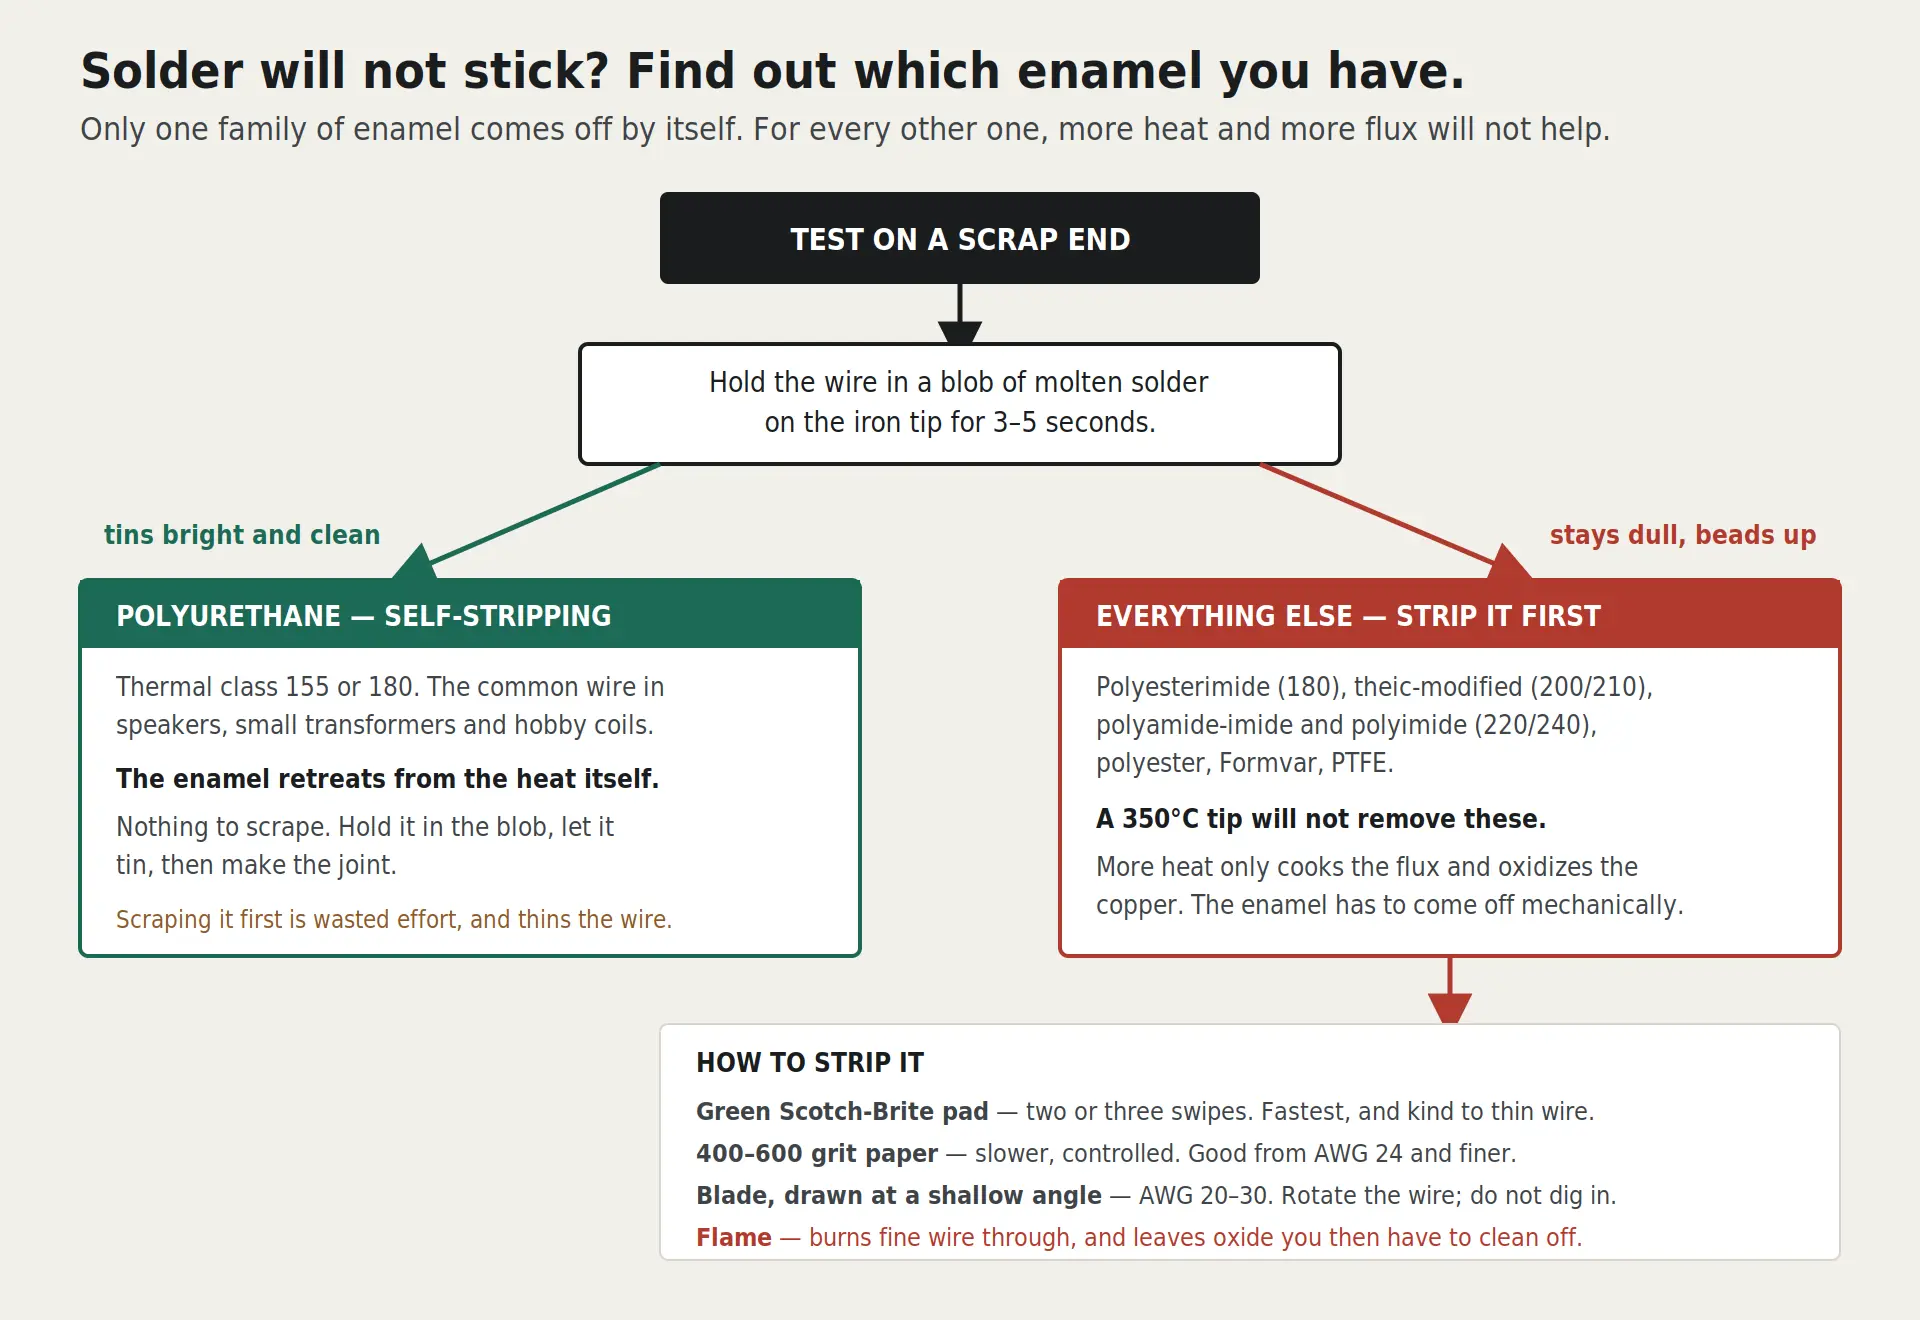
If the wire tins bright and clean, you have polyurethane enamel and there is nothing to strip. If the solder stays dull and beads up, the coating is one of the tougher families and no amount of heat will shift it.
Which Enamel You Have
| Enamel | Thermal class | Solder straight to it? | Where you find it |
|---|---|---|---|
| Polyurethane | 155, 180 | Yes — the coating retreats from the heat | Speaker voice coils, small transformers, most hobby magnet wire |
| Polyesterimide | 180 | No. Manufacturers state plainly it is not for direct soldering | Motor windings, better-quality coils |
| Theic-modified polyesterimide | 200, 210 | No | Hotter-running motors |
| Polyamide-imide, polyimide | 220, 240 | No. Industrially these need a salt bath | High-temperature and high-reliability windings |
| Polyester, Formvar | — | No. Scrape it | Older equipment, vintage radios, guitar pickups |
| PTFE | — | No. Mechanical removal only | Specialist high-temperature wire |
The number that explains the frustration. Leaded solder melts around 361°F (183°C) and lead-free around 423°F (217°C), and a typical iron tip runs near 660°F (350°C). That is hot enough to melt solder and nowhere near hot enough to remove most of these coatings. Turning the iron up does not close that gap — it just cooks the flux and oxidizes the copper, which makes the joint worse.
What You’ll Need
- Soldering iron, 40–60 W — copper pulls heat away fast, so an underpowered iron never gets the joint hot enough
- Flux-cored solder, or plain solder plus a pot of flux
- Green Scotch-Brite pad or 400–600 grit paper — only if the test says you need to strip
- Soldering stand and a damp sponge or brass wool for the tip
- Helping hands or a clamp — fine wire will not hold still
- Heat-shrink tubing, slid on before you solder
- Isopropyl alcohol and a brush to clean flux off afterwards
- Safety glasses and ventilation
The smoke off a soldering joint is flux, not lead — and it is the part that harms you
People worry about lead and ignore the smoke. Lead is a contact and ingestion risk, handled by washing your hands. The visible fumes are burning rosin flux, and repeated exposure to those is a known cause of occupational asthma. Burning enamel off wire adds its own decomposition products on top.
- Ventilate, and keep your head out of the plume. A small fan pulling air across the bench and away from you is enough, and costs almost nothing.
- Wash your hands before eating if you use leaded solder. Do not eat or drink at the bench.
- Safety glasses. Flux spits, and flicking excess solder off a hot iron sends droplets further than you would think.
- The iron looks identical hot and cold. It goes in the stand every single time, not on the bench.
- Do not burn enamel off indoors with a flame. It is the crudest method and the one that fills the room with decomposition fumes.
How to Solder an Enameled Wire
- Run the five-second test on a scrap end, so you know whether you are stripping or not.
- Strip only if the test said to. Two or three swipes with a green Scotch-Brite pad, or 400–600 grit paper, rotating the wire so you take the coating off all the way round rather than flattening one side. On heavier wire, AWG 20 to 30, a blade drawn along at a shallow angle works — draw it, do not dig in.
- Slide the heat-shrink on now. Every soldering guide says this and everyone still forgets. It cannot go on after the joint is made.
- Clean and tin the iron tip. A dull, crusted tip transfers heat poorly, and that alone is behind a lot of failed joints.
- Tin the wire. Hold it in a blob of molten solder on the tip until the solder flows onto the copper and coats it evenly. With polyurethane you will see the enamel give way as it heats. This is where you find out whether the preparation worked, before anything is committed.
- Tin the other side too — the pad, terminal or second wire.
- Bring the two tinned parts together and touch the iron to them. They should flow into one joint almost instantly, because the solder is already there. Hold it still for a second or two as it cools.
- Look at the joint. Bright and slightly concave is right. Dull, grainy or ball-shaped means it moved while cooling, or it never got hot enough — reheat it properly rather than adding more solder on top.
- Shrink the tubing and clean the flux residue off with isopropyl alcohol. If the joint has to carry a signal, check it with a multimeter on continuity before you seal anything up — a joint that looks right and reads open is almost always enamel left under the solder.
Tin both sides first, then join them. Trying to strip, flux, heat and join all in one go on a wire this thin is how people end up melting the insulation back along the coil or lifting a pad off a board. Two small operations beat one awkward one.
Why Enameled Wire Is Used at All
Worth knowing, because it explains why the coating is so stubborn. Ordinary plastic insulation is thick. Enamel is a film, which means turns of wire can sit against each other with almost no wasted space — so a coil of enameled wire is smaller, lighter and more efficient than the same coil in sleeved wire.
To survive being wound tight, heated by its own current and varnished into a motor, that film has to be tough and heat-resistant. The thermal class in the table is exactly that: the temperature the coating is rated to live at. A 240-class polyimide is built to shrug off heat continuously, which is precisely why a 660°F iron tip does nothing to it. The property that makes the wire good is the property that makes it hard to solder.
What I’d buy for this job


Last update on 2026-10-20 / Affiliate links / Images from Amazon Product Advertising API
Enameled Wire Soldering Questions People Actually Ask
Why won’t my solder stick to the wire?
Nine times out of ten the enamel is still there. Run the five-second test on a scrap end: if it beads up, you have a coating that will not self-strip, and the fix is mechanical removal rather than more heat. The other causes are a dull untinned iron tip, an underpowered iron, or no flux.
Can I use sandpaper to strip the enamel?
Yes, and it is a good method — but use 400 to 600 grit, not coarse paper. Coarse abrasive removes copper along with the coating, and on fine wire that means a thinner conductor and a weak spot. Rotate the wire so you take the enamel off the whole circumference. A green Scotch-Brite pad is faster and gentler still.
Can I burn the enamel off with a lighter?
You can, and it is the method I would reach for last. Flame burns straight through fine wire, it leaves an oxide layer you then have to clean off before the solder will take, and it fills the room with decomposition fumes. Use it outdoors on heavy wire, or not at all.
What wattage soldering iron do I need?
40 to 60 W for general work. Copper carries heat away from the joint quickly, so a low-powered iron ends up parked on the wire for a long time — which melts more insulation back along the wire than a hotter, faster joint ever would.
Can I re-solder a joint that looks bad?
Yes. Reheat it until the solder is fully molten, and lift the excess away with solder wick or a sucker. Then re-flux and do it again. Adding fresh solder on top of a cold joint without remelting the old is what leaves you with a lumpy connection that fails later.
How do I know the joint is good?
It should be bright and slightly concave, with the wire outline visible through the solder. Dull and grainy means it moved while cooling. Round and beaded means it never wetted the metal properly — usually enamel still in the way.
Does the wire need cleaning before soldering?
If it is old, yes — oxide and fingerprint oil both stop solder wetting. Isopropyl alcohol and a wipe is enough. On new wire off the spool, the enamel is the only thing in the way.
Getting a Clean Joint
Test the wire before you commit to a technique, strip it only if it needs stripping, tin both sides separately, and bring them together with an iron that is hot enough to work fast. The frustration almost always comes from doing the right procedure on the wrong kind of wire.